D- Ribose Bulk


2.Appearance:White Crystalline Powder
3.Specification: 99% HPLC
4.CAS NO: 50-69-1
5.Packing Specification: 25kg/drum, 27 drums/tray
6.Delivery: 3-7working days
7.Certification: cGMP,KOSHER,HALAL,BRC,ORGANIC,ISO9001,ISO22000 etc.
8.Main Market: European, North America, Asia
D‑Ribose Bulk Powder | Fermentation‑Derived Nutraceutical & Pharmaceutical Intermediate Raw Material
We supply bulk fermentation‑produced D‑Ribose bulk crystalline powder for nutraceutical, functional‑food and pharmaceutical intermediate projects. Many formulators reach out to us with practical concerns around hygroscopic behaviour, optical rotation verification and lot‑to‑lot consistency.
We offer food‑grade and pharma‑grade specifications. Every finished lot comes with lot‑tied COA, HPLC assay report, optical‑rotation reading, heavy‑metal and full microbial screening data. Evaluation samples and independent ISO‑17025 third‑party testing are available for manufacturers and ingredient distributors across global markets.

D- Ribose Bulk Introduction
D-ribose powder is a naturally occurring five-carbon sugar that is a key component of adenosine triphosphate production in cellular energy pathways. This pentose monosaccharide is the core structure of nucleotides, and, unlike typical glucose sources, is not used as the main fuel source. Therefore, it is vital for cardiac and skeletal muscle recovery applications. Our fermentation-derived material is characterised by a consistent crystalline structure and excellent water solubility, allowing manufacturers to overcome formulation hurdles in sports nutrition and cardiovascular health products where rate-limiting biosynthesis results in supply shortages in stressed tissue.
Product Advantages
Pharmaceutical-Grade Purity: Our fermentation technique yields constant 99%+ purity, removing competing sugars and metabolic interference for predictable ATP regeneration in your final products.
Improved Physical Properties: Moisture content is controlled to less than 1% to avoid clumping during shipping and storage. Particle size distribution is uniform to allow for uniform mixing in complicated supplement matrices without segregation problems.
Verified Optical Activity Specific rotation testing between +19° and +21° shows the presence of just D-isomer content, the physiologically active form for nucleotide synthesis routes that generic suppliers cannot guarantee.
Non-GMO Fermentation Source: Bacillus subtilis fermentation of proven non-GMO maize glucose makes for a product that meets clean label demands, stays vegan-friendly and allergen-free for global market access.
Specifications
|
Item
|
Specification
|
Test result
|
|
Physical Contro
|
||
|
Appearance
|
White Crystalline Powder
|
Conforms
|
|
Odor
|
Characteristic
|
Conforms
|
|
Taste
|
Characteristic
|
Conforms
|
|
Purity
|
99%
|
Conforms
|
|
Loss on Drying
|
≤5.0%
|
Conforms
|
|
Ash
|
≤5.0%
|
Conforms
|
|
Particle size
|
95% pass 80 mesh
|
Conforms
|
|
Allergens
|
None
|
Conforms
|
|
Chemical Control
|
||
|
Heavy metals
|
NMT 10ppm
|
Conforms
|
|
Arsenic
|
NMT 2ppm
|
Conforms
|
|
Lead
|
NMT 2ppm
|
Conforms
|
|
Cadmium
|
NMT 2ppm
|
Conforms
|
|
Mercury
|
NMT 2ppm
|
Conforms
|
|
Microbiological Control
|
||
|
Total Plate Count
|
10,000cfu/g Max
|
Conforms
|
|
Yeast & Mold
|
1,000cfu/g Max
|
Conforms
|
|
E.Coli
|
Negative
|
Negative
|
|
Salmonella
|
Negative
|
Negative
|
Important manufacturing note: For manufacturing and laboratory use only. Not intended for direct consumer intake.
D- Ribose Bulk Use
Advanced Sports Nutrition Formulations: Present in pre-workout powders and post-recovery powders where it allows rapid resynthesis of adenyl nucleotides after strong anaerobic activity, especially when combined with creatine monohydrate to increase ATP availability.
Cardiovascular Health Products: Employed in therapeutic nutrition formulas for congestive heart failure and fibromyalgia treatment, enhancing diastolic function and cellular energy levels in impaired cardiac tissue, with rigorous adherence to pharmacopeial compliance.
Functional Beverage Development: Used as a low glycaemic energy modulator in ready to drink beverages and energy gels. Formulation needs precise pH management and heat processing controls to minimise Maillard reaction browning during pasteurisation.

Production Process
Step 1 - Strain Selection and Fermentation: Proprietary cultures of Bacillus subtilis are grown on sterile glucose medium under regulated temperature and pH conditions. This gives bio-identical D- Ribose from D- Ribose Bulk using enzymatic conversion mechanisms.
Step 2 – Separation and Purification: The fermentation broth is subjected to membrane filtration and activated carbon treatment to remove cellular debris and fermentation by-products. This provides a clarified ribose solution that meets the original purity standards.
Step 3 – Crystallisation and drying: The concentrated solution is crystallised under controlled conditions and vacuum dried in GMP-certified chambers. Moisture concentration below 1% is targeted with no damage to the crystalline structure.
Step 4 – Quality Testing and Packaging The final substance is subjected to extensive testing using HPLC, ICP-MS and microbiological methods. When the material passes these tests it is packed in double walled PE bags and placed in fibre drums which include desiccants to protect the item from moisture during transport.\
Report of Third Party Test
Independent Laboratory Testing: Our D-Ribose is subject to strict third party testing by SGS and Eurofins labs to confirm quality criteria beyond our in-house testing procedures.
Purity confirmation: HPLC analysis always confirms 99.0-101.0% test values on a dry basis, with no fermentation byproducts or other sugar impurities diluting bioactivity.
Heavy Metal Screening: ICP-MS testing shows lead concentration less than 0.5ppm, arsenic less than 0.5ppm, mercury and cadmium satisfy the most stringent international guidelines for use in dietary supplements.
Microbiological Safety: Total plate counts < 1000 CFU/g, Yeast and Mould < 100 CFU/g, Pathogen Testing – no Salmonella or E. coli was detected in any of the manufacturing batches.

Why Choose Us
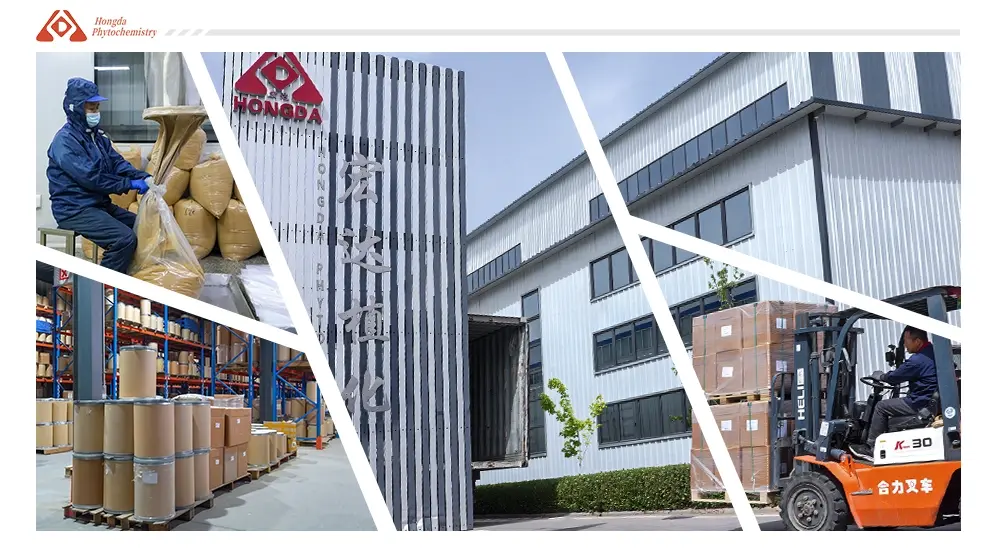
Shaanxi Hongda was founded in 2001 and is a national high-tech firm with advantages of vertical integration and strict quality processes. We have 3 specialised planting bases to assure traceability of raw material and our SGS standardised labs with HPLC, GC and spectrophotometry provide real-time quality verification. We are certified with the likes of cGMP, FSSC22000, ISO22000, HALAL, KOSHER and ORGANIC certified to help us enter the worldwide market. We have 150+ technical operators and professor level researchers, providing not just ingredients, but comprehensive technological collaborations. Our 3,000 square meters of warehouse space and significant stock in 6 specialised areas offer a regular supply and quick service without disrupting your production plans.

OEM/ODM Support
Custom Formulation Development: Our 20-member R&D team works with your product development professionals to build optimised mixes using D-Ribose and complementing substances such as creatine, beta-alanine or CoQ10 for targeted performance results.
Flexible Dosage Forms: We develop tailor-made products such as soft capsules, hard capsules, tablets, premixed powders, and ready-to-drink concentrates, all manufactured in our 100,000-level purification factories with tight contamination controls.
Regulatory Documentation Help: Complete regulatory dossiers include stability studies, allergy declarations and regulatory compliance documents for FDA GRAS status and EU Novel Food approvals, accelerating your time-to-market across foreign regions.
manufacturing Capacity: We can produce 3,000 tonnes per year on 10 of the most advanced manufacturing lines, which enables us to complete requests from research batches to full commercial supply with constant quality criteria.

Packaging, MOQ & Lead Time
Packaging
‑ Evaluation sample unit: Moisture‑barrier vacuum‑sealed foil pouch ‑ Bulk shipment: 25kg moisture‑proof fiber‑drum fitted with dual food‑grade inner plastic bags. Custom labels are available on large‑volume orders.
Order Information
‑ Evaluation sample:100‑500g for lab formulation assessment ‑ MOQ:1kg for trial batch; 25kg for standard bulk shipment ‑ Sample lead‑time:4‑6 working days ‑ Bulk production lead‑time:8‑16 working days, subject to production scheduling and order scale ‑ Shipping options: Air express for small consignments; sea‑freight for bulk‑volume orders
Practical business note: For large multi‑ton orders, please send inquiry ahead so we can lock production slot and stabilise batch consistency for you.
FAQ
Q: Is your product compatible with protein-based formulations?
A: Yes, though D-Ribose can trigger Maillard browning reactions when exposed to heat with proteins. We recommend encapsulation techniques or strict temperature controls during processing to maintain product appearance.
Q: What measures prevent moisture-related quality degradation?
A: Our storage is temperature controlled and relative humidity is maintained at below 60%. We use double-lined packing and desiccants. Our regulated Loss on Drying requirements provide free-flowing material throughout shelf life.
Q: Do you have organic or particular certification documentation?
A: Yeah, for sure. Our plant is certified ORGANIC (EU and NOP) and has complete regulatory paperwork to support GRAS status in North America and Novel Food compliance throughout the European marketplace.
Q: How does your product solve for cardiovascular applications?
A: Clinical studies have shown that ribose supplementation enhances the diastolic function of the heart by replenishing depleted adenine nucleotide pools in the heart tissue and is especially advantageous if the cardiovascular system is damaged.
Q: What are your minimum order quantities?
A: Our usual packing is 25kg drums and we ship 27 drums per pallet. We are also happy to provide smaller trial orders to help your product development phase before scaling up to commercial production numbers.
Ready to enhance your formulations with pharmaceutical-grade D- Ribose Bulk? Contact Duke at duke@hongdaherb.com for detailed specifications, pricing information, and sample requests.
Special Note
Our D‑Ribose comes from strictly‑controlled microbial fermentation, followed by multi‑stage filtration, ion‑exchange purification and low‑temperature crystallization. Intermediate sampling happens through the whole production cycle; testing is not limited to finished crystalline powder at final step.
Each finished lot goes through complete in‑house testing covering HPLC assay, optical rotation, moisture, heavy‑metal and microbial screening. Retained reserve samples are preserved for every production batch for retrospective review.